Some materials refuse to grind warm
Most powders get finer the way you would expect. Feed them into a mill, hit them hard enough, and they break. A whole class of materials does something else. Rubber stretches instead of fracturing. Many plastics and waxes soften from the heat the mill itself generates, smear across the grinding surfaces, and blind the screen. Resins with a low softening point turn tacky and fuse back into lumps. Products with volatile components lose part of what makes them work before they ever leave the mill.
Push harder on any of those materials at room temperature and you just make more heat, which makes the problem worse. The fix is to take the heat out of the equation entirely. That is what cryogenic grinding does.
What cryogenic grinding is
Cryogenic grinding chills the material to a very low temperature before and during size reduction, so it behaves like glass instead of chewing gum. Elastic and soft materials become brittle when they are cold enough, and brittle material shatters cleanly under impact. The cold also carries away the heat of grinding as it forms, so the product never reaches the temperature where it would soften or degrade.
Lab mill maker Retsch describes the usual grinding aids as "liquid nitrogen (-196 °C) or dry ice (-78 °C) which embrittle the sample by cooling and make it break more easily." Its guidance adds that for a successful size reduction the temperature of the sample must not exceed its glass transition temperature, the point where a polymer shifts from rubbery to glassy. Retsch also notes a second benefit: the low temperature substantially reduces the vapor pressure of volatile components, so they stay in the product.
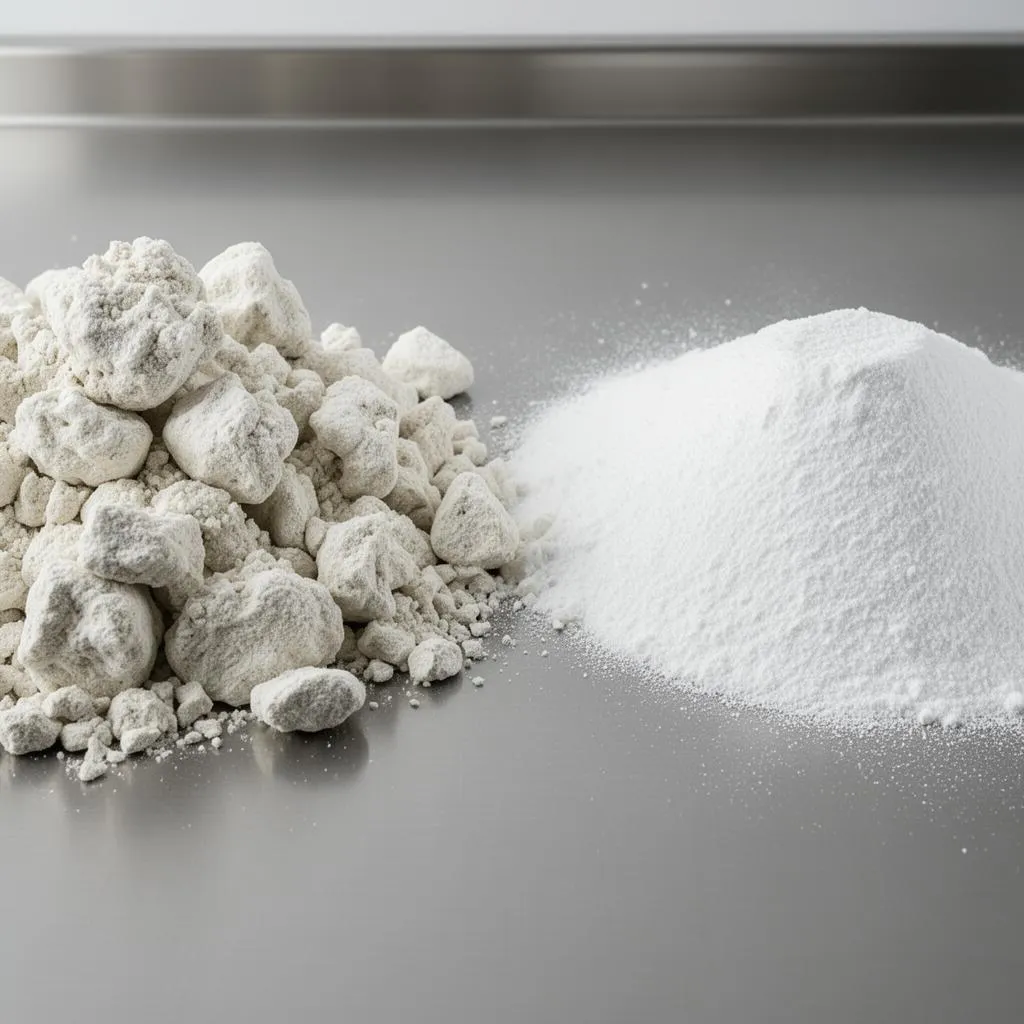
Liquid nitrogen is the common cryogen because it is about as cold as industrial practice gets. The NIST Chemistry WebBook lists nitrogen's boiling point at 77.34 K, and it boils off as an inert gas, which also blankets the mill and keeps oxygen away from the product while it is being ground.
Materials that usually need it
- Rubbers and elastomers, which deform instead of breaking at room temperature.
- Thermoplastics and polymer additives with low softening points.
- Waxes and waxy additives that melt or smear under friction.
- Resins that turn sticky as they warm.
- Products where a volatile component, an aroma, or a solvent residue has to survive the process.
- Materials that oxidize or discolor when ground hot.
Not every heat-sensitive product needs the full cryogenic treatment. Sometimes a different mill, a slower feed, or chilled process air is enough. The deciding question is whether the material can reach your target particle size without passing its softening or degradation point. If it cannot, cold is the tool.
Cryogenic grinding vs. jet milling vs. standard grinding
We run all three under one roof, and they solve different problems. Here is how they compare in practice.
| Method | How particles break | Best for | Heat into product |
|---|---|---|---|
| Standard grinding | Mechanical impact or shear | Coarser targets, brittle materials | Moderate |
| Jet milling | Particle on particle collisions in high velocity air | Ultra-fine targets, single-digit microns | Low |
| Cryogenic grinding | Impact on embrittled, chilled material | Elastic, soft, or heat-sensitive materials | Removed by the cryogen |
Jet milling deserves a note here, because it is also gentle on heat. It uses compressed air or gas to slam particles into each other with no grinding media, which makes it the right call for a brittle material that needs to go very fine. It does not help a material that is rubbery to begin with. Our jet milling and micronization explainer covers that side in more depth.
How a cryogenic grinding run works
- Pre-cooling. The material is chilled to below its embrittlement point, either in a pre-cooler ahead of the mill or by introducing the cryogen into the feed.
- Grinding. Cold, brittle feed goes into the mill, where impact breaks it down. The cryogen keeps absorbing the heat the mill generates.
- Classification. Ground product is screened or classified so oversize goes back for another pass and the finished fraction meets the target cut.
- Warm-up. Cold powder pulls moisture out of the air as it warms. Product should come up to ambient temperature in a closed container before it is packed, or it can condense water on itself and cake later.
- Packaging. The finished powder goes into whatever package the job calls for, from small bags to super sacks.
That warm-up step is the one people skip, and it is behind a lot of complaints about cryo-ground product clumping in the bag a month later. If your material is moisture sensitive to begin with, plan for it. Our guide to storing and packaging hygroscopic powders has the packaging side.
What drives cost and turnaround
Cryogenic grinding costs more per pound than grinding at room temperature, and the reasons are straightforward. The cryogen is consumed as the job runs, so throughput matters a great deal: a material that grinds quickly once it is cold uses far less cryogen per pound than one that needs several passes. A finer target means more passes and more screening. Small development batches carry setup cost that larger campaigns spread across more pounds.
The cheapest way to find the real number is a trial. A small run tells you how the material breaks, what particle size distribution comes out, and what the yield looks like at your target cut. From there the production quote is based on the material's actual behavior instead of a guess. We quote same day, most projects start within 48 hours of material arriving at our Elyria, Ohio facility, and standard turnaround runs 3 to 5 days with rush options available.
When you reach out, the useful things to have ready are the safety data sheet, your target particle size or distribution (a D50 and a top cut are ideal, and our guide to D10, D50, and D90 explains how to write one), the quantity, and the package you want back. See the full list of size reduction options on our jet milling and grinding services page.
Frequently asked questions
What is cryogenic grinding?
Cryogenic grinding is size reduction done at very low temperature, usually with liquid nitrogen. Chilling makes elastic or heat-sensitive materials brittle so they shatter cleanly, and the cold carries away the heat of grinding so the product does not soften, melt, or lose volatile components.
When does a material need cryogenic grinding instead of standard grinding?
When it cannot reach the target particle size without softening, smearing, melting, or degrading from mill heat. Rubbers, many thermoplastics, waxes, low-softening resins, and products with volatile components are the usual candidates.
Is cryogenic grinding more expensive?
Yes, per pound, because the cryogen is consumed during the run and throughput is often lower. The gap shrinks for materials that grind quickly once cold, and a small trial run is the best way to get a real production price.
How fine can cryogenic grinding go?
It depends on the material and how many passes and classification steps are used. For ultra-fine targets on brittle materials, jet milling can reach single-digit microns, and some projects combine methods to hit both the size and the heat limits.
Where can I get cryogenic grinding done in Ohio?
U.S. Chemical Services offers cryogenic grinding, jet milling, and standard grinding at its 100,000 sq ft facility at 955 Taylor St in Elyria, Ohio, serving customers across North America. Call (440) 529-8868 for a same-day quote.
How long does a cryogenic grinding project take?
Most projects start within 48 hours of material arriving, and standard turnaround is 3 to 5 days, with rush options when a production schedule is waiting. A small trial batch runs on the same timeline.
Need help with your chemical processing project?
Talk to our team today. Most projects start within 48 hours of receiving materials.